Founded in 2010, FLYPOWER is a high-tech enterprise specializing in the research, development, production, and sales of polymer materials. Leveraging its core technological strengths and starting with heat-shrink materials, the company established its Medical Division in 2018, expanding its business and product portfolio into the fields of medical devices and catheters, with the mission of becoming a globally leading supplier of materials for interventional medical devices.
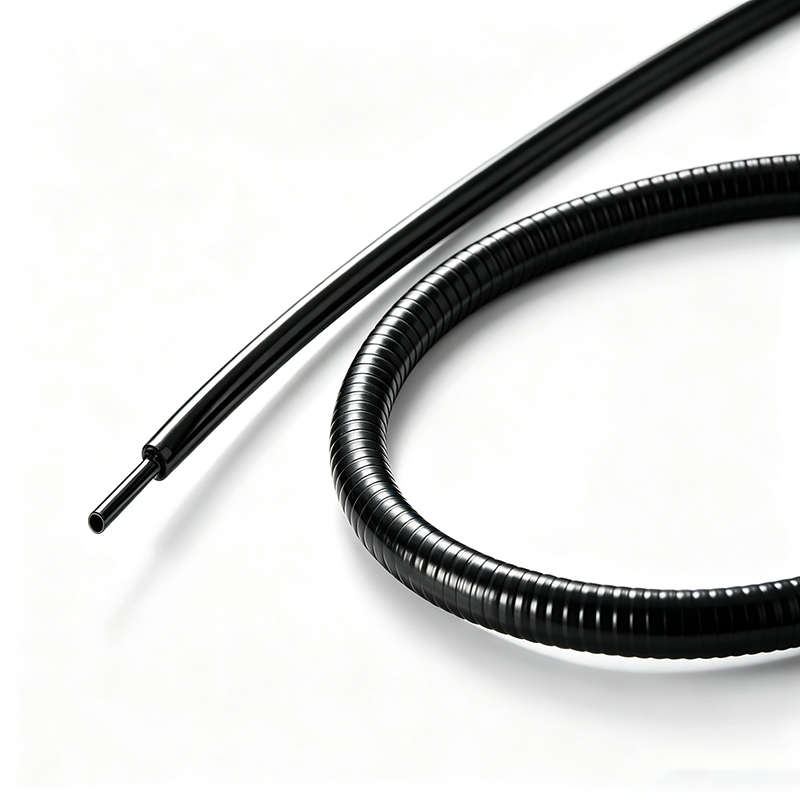
联系我们 No. 77, Bao Nan Road,Nan Lian Community,Long Gang Street,Long Gang District, Shenzhen, Guangdong,518116,China (+86)755 2917 9250 [email protected]BH-MT-2-F delivers superior flexibility and is engineered to provide insulating protection for medical devices requiring pliability and bend resistance. Its low-temperature shrink characteristic minimizes damage to heat-sensitive components.
Shrink ratio: 2:1 or higer
Low shrink temperature
Very flexible
Good physical, chemical, and electrical properties
Excellent electrical insulation properties
Compatibility with gamma rays and ETO sterilization
Operating temperature: -55˚C~105˚C
Minimum shrink temperature: 60℃
Minimum fully recovery temperature: 110℃
ISO 10993, USP Class VI and RoHS compliant
|
Model |
Supplied |
Recovered(mm) |
Package (Meters/Spool) |
||
|
Mini. ID |
W.T |
ID |
W.T |
||
|
BH-MT-2-F-1.2 |
1.2 |
0.20±0.05 |
≤0.6 |
0.41±0.08 |
200 |
|
BH-MT-2-F-1.6 |
1.6 |
0.20±0.05 |
≤0.8 |
0.43±0.08 |
200 |
|
BH-MT-2-F-2.4 |
2.4 |
0.25±0.05 |
≤1.20 |
0.51±0.08 |
200 |
|
BH-MT-2-F-3.2 |
3.2 |
0.25±0.05 |
≤1.6 |
0.51±0.08 |
200 |
|
BH-MT-2-F-4.8 |
4.8 |
0.25±0.05 |
≤2.40 |
0.51±0.08 |
100 |
|
BH-MT-2-F-6.4 |
6.4 |
0.30±0.05 |
≤3.2 |
0.64±0.08 |
100 |
|
BH-MT-2-F-9.5 |
9.5 |
0.30±0.05 |
≤4.8 |
0.64±0.08 |
100 |
|
BH-MT-2-F-12.7 |
12.7 |
0.30±0.05 |
≤6.40 |
0.64±0.08 |
100 |
|
BH-MT-2-F-19.1 |
19.1 |
0.35±0.05 |
≤9.5 |
0.76±0.08 |
50 |
Customized dimensions and heat shrink ratio for your special applications on request.
|
Property |
Test Method |
Typical Data |
|
Longitudinal change % |
ASTM D 2671 |
-10~+10 |
|
Concentricity |
ASTM D 2671 |
≥70% |
|
Tensile strength/MPa |
ASTM D 638 |
≥10.3 |
|
Elongation at break/% |
ASTM D 638 |
≥120 |
|
Low temperature flexibility(-55°C/4h) |
ASTM D2671 |
No cracking |
|
Heat shock(180˚C/4 h) |
ASTM D2671 |
No cracking |
|
Dielectric strength/kV/mm |
ASTM D 2671 |
≥19.7 |
|
Volume resistivity/Ω·cm |
ASTM D 876 |
≥1015 |
Written for medical device R&D and process engineers, OEM/ODM partners and sourcing teams working on flexible medical devices, articulated instruments, cable assemblies and other medical equipment that must bend in service. This FAQ focuses on selection, thermal processing practice, failure modes, substrate compatibility, sterilization, compliance boundaries, storage, secondary processing, qualification ramp and sourcing. All physical properties, dimensions, shrink ratio and test values are published in the product datasheet and are intentionally not repeated here — refer to the BH-MT-2-F product page for the full specification.
1. Selection & Pre-checks
Q1. What should we verify before selecting BH-MT-2-F for a flexible or bend-critical application?
A1. BH-MT-2-F is the high-flexibility thin-wall grade of the family, engineered for insulating protection on devices that need pliability and bend resistance. Verify four checkpoints.
(1) Fit at both states: the supplied ID must slide over your component freely, and the recovered ID must grip with positive interference — cross-check the datasheet size bands against your drawing, not just the nominal size name.
(2) Bend geometry: flexibility is not unlimited — check the minimum bend radius in your design against the recovered sleeve on your actual build; a bend radius that is too tight for the combination of recovered wall and underlying component leads to kinking regardless of material flexibility.
(3) Profile budget: on a thin-wall grade, the recovered-wall tolerance directly consumes your OD envelope, so confirm the band, not the nominal.
(4) Process prerequisites: this grade recovers at low temperature (see datasheet) and its low-temperature shrink characteristic minimizes damage to heat-sensitive components — but you still need controlled, uniform heating equipment; plan that before design freeze, and request evaluation samples to run trials on your real assembly.
Q2. Which heating equipment suits this tubing, and what failure modes should we watch for?
A2. Use validated convection ovens, automated hot-air rings or infrared stations with closed-loop temperature control and fixed feed rates. Handheld heat guns are the leading cause of scrap and latent field failures: hot spots locally over-shrink or degrade the polymer while adjacent zones remain unrecovered, and results become operator-dependent — unacceptable in a validated medical process. When shrinking over heavy metal parts, pre-heat the core so the sleeve is not heat-sinking on the inside. Failure modes frequently reported with flexible thin-wall medical sleeves:
(1) cracking or splitting — initiated at sharp edges, burrs or steps, or driven by thermal peaks and excessive heat exposure that degrades and embrittles the polymer; deburr all edges and stay inside the qualified process window;
(2) whitening or chalky marks — stress whitening from over-stretching during installation, kinking, or excessive local strain; a rejectable defect signaling damaged polymer and a future crack-initiation site;
(3) bubbles or blisters — air trapped at the ends or too-rapid heating; shrink progressively from one end to the other in a single smooth pass so air escapes;
(4) uneven recovery or waviness — non-uniform heating; rotate the part or use 360° heating;
(5) kinking or collapse on soft substrates during processing — when shrinking over very soft components, an internal support mandrel during recovery prevents permanent collapse; (6) longitudinal shift — this family changes length during recovery (see datasheet), so position with allowance and verify end positions on first articles.
Q3. What should we know about contact with device substrates, metals and medical adhesives?
A3. The low recovery temperature makes this tubing friendly to mixed-material builds — it can typically be recovered over stainless steel, Nitinol and many thermoplastic constructions (PEBAX, Nylon, PU) without damaging them, but verify on your exact stack since softening behavior varies widely by grade and durometer. Over metals, surface condition is the hard precondition: deburr, polish or tumble every edge, weld seam and step the sleeve will cross — a sharp feature under recovery hoop stress becomes a crack-initiation site, and in a flexing application repeated motion turns it into a through-crack. Keep contact surfaces clean — machining oils, polishing compounds and unflashed isopropanol residues degrade recovery quality and seed blisters. On adhesion: this is a low-surface-energy polyolefin — medical adhesives, primers and overmolding materials will not bond reliably to it without surface treatment (corona, plasma or chemical primer). If your design bonds or overmolds over the sleeve, plan that step explicitly or contact us to discuss options.
Q4. Any precautions for chemicals and disinfectants, and what declarations are available?
A4. The tubing tolerates routine hospital cleaning and common disinfectants, but two cautions matter on flexible builds. First, polyolefins are less chemically inert than fluoropolymers: avoid prolonged contact with strong oxidizing agents and aromatic or chlorinated solvents. Second, watch environmental stress cracking: aggressive disinfectant exposure on a sleeve section that is simultaneously under bending stress — a wiped-down handle-to-cable junction, for example — is the classic combination that accelerates surface crazing and cracking over the device lifetime; if your device sees frequent disinfection at flex points, include that combination in your validation. If a specific chemistry is unavoidable, share the agent, concentration and exposure cycle with us and we will support a compatibility assessment. On documentation: the material complies with ISO 10993, USP Class VI and RoHS (see datasheet), and we support your material-declaration work with composition statements and material test reports. Raise any substance-level declaration needs (SVHC, REACH, specific restricted substances) in the RFQ so the correct documentation is prepared from the start.
Q5. Which sterilization methods are supported, and what changes should we expect with repeated cycles?
A5. The datasheet states compatibility with gamma irradiation and ethylene oxide (EtO) sterilization. Two honest boundary notes.
(1) Steam autoclaving and dry-heat sterilization are not supported by this material family: the material’s operating range (see datasheet) is far below autoclave conditions, and a steam cycle will distort or re-shrink the recovered sleeve — if your device requires steam reprocessing, ask us about higher-temperature grades instead.
(2) Even with the qualified methods, validate on the recovered sleeve on your actual device across the full intended cycle count: repeated radiation or EtO cycles can shift polyolefin properties, and on a flexible application you should verify not only dimensional stability, surface condition and grip, but also retained flexibility and — where the sleeve serves as insulation — dielectric integrity after exposure, since stiffening or embrittlement shows up first at the bend points. Include the worst-case cycle number in your validation plan rather than a single pass.
Q6. Where is BH-MT-2-F the right choice — and where is it NOT recommended?
A6. Well suited: insulating protection and light strain relief on medical devices that must bend in service — flexible device sections, articulated instrument zones, cable-to-connector transitions and cable assemblies — wherever pliability and bend resistance are required, processed with gentle low-temperature heat, and where electrical insulation performance is needed. Use with caution or not recommended: devices that will undergo steam autoclaving or dry-heat reprocessing (see the sterilization question); continuous service above the rated operating range (see datasheet); applications expecting the sleeve to carry structural, tensile or torsional load — it is an insulating jacket, not a structure; bend radii tighter than the recovered sleeve can follow without kinking — if the transition stiffness jump is the real problem, consider a tapered or stepped strain-relief design rather than relying on one sleeve; assemblies with sharp edges that cannot be smoothed; and severe sliding abrasion. Note also that flexibility and abrasion resistance trade off against each other: if your application is dominated by mechanical wear, high temperature or aggressive chemicals, tell us before design freeze and we will point you to the right grade in our range.
Q7. Does ISO 10993 / USP Class VI compliance — or the published dielectric rating — mean our finished device is approved?
A7. No — and this distinction matters in audits. We supply component tubing only. Material-level compliance with ISO 10993 / USP Class VI supports, but does not replace or constitute, regulatory approval of your finished medical device: biological evaluation of the finished device (ISO 10993-1), sterilization validation, process validation (IQ/OQ/PQ) and risk analysis (ISO 14971) remain the device manufacturer’s responsibility. The same logic applies electrically: the dielectric properties in our datasheet are material-level test values, not an electrical safety certification of your instrument. Dielectric withstand (hi-pot), leakage current, creepage and clearance verification on the finished device (for example under the IEC 60601 series where applicable) must be performed and documented by you on the final assembly — including after sterilization, aging and flex cycling, because insulation performance can drift and a processing crack or kink defeats the material rating. We do not claim performance beyond the published datasheet.
Q8. How should the tubing be stored, and does long-term storage affect performance?
A8. Polyolefins are more storage-sensitive than fluoropolymers. Keep the tubing in its original packaging, cool, dry, away from direct sunlight/UV and heat sources: elevated storage temperature can slowly relax the expanded state and reduce available recovery, and UV/ozone ages polyethylene surfaces. Store spools and cut pieces so they are not kinked or crushed in the box — a sharp set from storage becomes a stress-whitened weak point on recovery. Apply first-in-first-out rotation. The datasheet does not assign a fixed shelf life; for lots stored long-term, run a quick recovery check on a sample piece at your qualified settings before releasing the lot to production, and include storage conditions in your incoming-inspection plan. For batch-to-batch consistency assurance on a running program, agree a retained-sample and lot-traceability scheme with us at the supply-agreement stage — it is the cheapest insurance against incoming-material risk.
Q9. Do you support cutting, custom dimensions, custom colors or special shrink ratios?
A9. Cut-to-length supply is supported, and cut quality is a functional requirement, not a cosmetic one: dull blades and shears leave micro-nicks and jagged rims that act as crack-initiation sites under recovery hoop stress and subsequent flexing, so we cut with sharp, dedicated tooling and inspect edges — if you cut in-house, hold the same standard. Standard colors are black and clear, with other colors available on request; customized dimensions and shrink ratios can be discussed for special applications (see datasheet). Marking and similar secondary operations can be evaluated on request — tell us the requirement in the RFQ and we will confirm feasibility and achievable tolerances. Given the family’s longitudinal change during recovery (see datasheet), also agree whether cut length is specified in the supplied or recovered state.
Q10. How do samples and the ramp from trials to mass production work?
A10. Evaluation samples of standard sizes are available so you can qualify the recovery window on your real equipment and components before any commitment — for a flexible application, use the sample stage to check not only recovery but the bend behavior of the finished joint: minimum bend radius without kinking, feel, and — where relevant — flex-cycle life on a representative assembly. We then support pilot batches through to mass production, with lead times confirmed at quotation. If you are dual-sourcing against an incumbent supplier, share the reference specification (dimensional class, recovered wall, color, performance requirements) and we will map the closest equivalent for side-by-side trials. Recommended practice for second-source introduction: keep incoming inspection of first production lots against your qualified reference samples, and retain golden samples from the qualification lots for later lot comparison.
Q11. What engineering information should an RFQ include?
A11. For a fast and accurate quotation, please provide: required size (supplied ID and/or recovered ID) and the recovered wall-thickness requirement, including which tolerance is functionally critical; quantity and estimated annual volume; supply form (spool or cut length, with tolerance, and whether length is defined in the supplied or recovered state); color; the application and what sits under the sleeve (component material, diameter range and tolerances, surface condition); the bend requirement (minimum bend radius in service, static or dynamic flexing, expected flex-cycle count); the profile budget the recovered sleeve may add; your heating equipment type and process temperature; whether the sleeve must be bonded to or overmolded (i.e., whether surface treatment is planned); sterilization method and number of cycles; electrical requirements if used as insulation (operating voltage, the finished device’s hi-pot level, and whether pinhole/continuity inspection is required); secondary operations (cutting, marking); compliance documentation required (ISO 10993 / USP Class VI material reports, RoHS and composition declarations); and target price, delivery terms and destination.
Q12. What should we know about material declarations, MAF files and change control?
A12. Practical points.
(1) We provide material-level documentation — composition statements, RoHS statement and ISO 10993 / USP Class VI material test reports — for your technical file, EU MDR documentation or supplier-qualification records.
(2) Where a device master file (MAF) reference is the right mechanism, we can discuss authorization letters so your regulatory team can reference our material data in your submission; scope is agreed case by case.
(3) What we do not do: we make no claim or commitment on behalf of your finished device — our material documents imply no device-level FDA clearance, no CE conformity, and no device-level biological or electrical safety approval.
(4) Change control: if your regulatory filing requires notification agreements for material or process changes, raise this before design freeze so it is covered in the supply agreement — second-source migrations and material changes are both reportable events in many device filings, and aligning notification duties in the contract is far easier than retrofitting them later.