Founded in 2010, FLYPOWER is a high-tech enterprise specializing in the research, development, production, and sales of polymer materials. Leveraging its core technological strengths and starting with heat-shrink materials, the company established its Medical Division in 2018, expanding its business and product portfolio into the fields of medical devices and catheters, with the mission of becoming a globally leading supplier of materials for interventional medical devices.
联系我们 No. 77, Bao Nan Road,Nan Lian Community,Long Gang Street,Long Gang District, Shenzhen, Guangdong,518116,China (+86)755 2917 9250 [email protected]
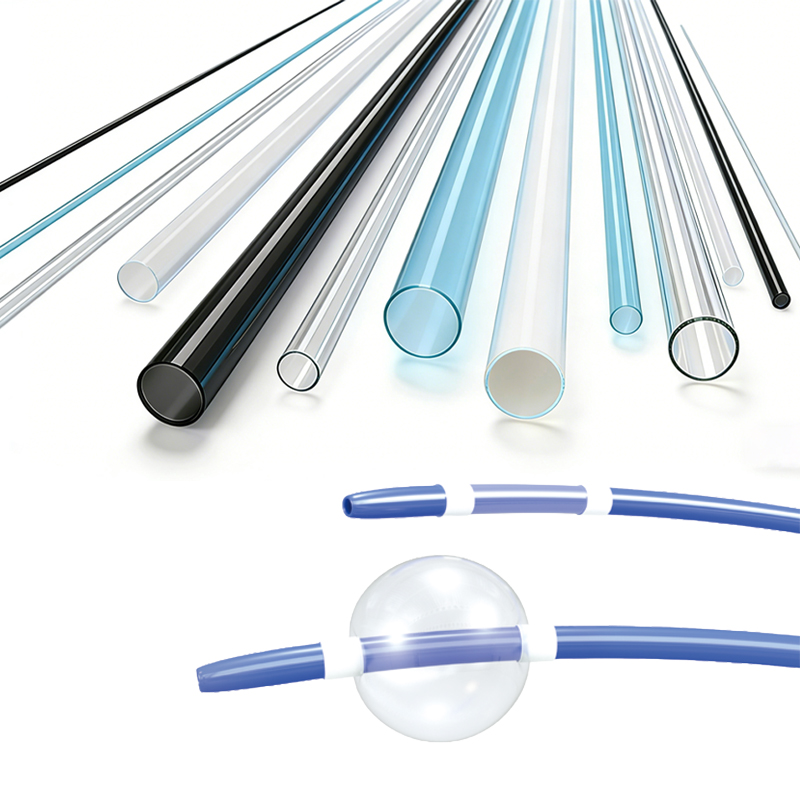
BH-MT-PTFE-UTW medical-grade ultra-thin-wall PTFE heat-shrink tubing is made of polytetrafluoroethylene (PTFE), It is widely used for coating, insulation, and smoothing modifications in precision minimally invasive devices such as microcatheters, balloon delivery systems, interventional guidewire sheaths, electrosurgical ablation electrodes, and endoscopic control wires.
Shrink ratio: 1.7:1
An ultra‑thin‑wall design, adding virtually no bulk to the device’s profile after heat shrinkage
low coefficient of friction
excellent resistance to corrosion by pharmaceutical solutions
resistance to high temperatures
Compatibility with high pressure, ETO, steam and dry heat sterilization
Operating temperature: -65℃~260℃
Minimum fully recovery temperature: 350℃
ISO 10993, USP Class VI compliant
|
Model # |
Min. ID |
Fully recovered ID(Max.) |
Fully recovered WT(Nor.) |
|||
|
In. |
mm |
In. |
mm |
In. |
mm |
|
|
BH-MT-PTFE-1.7X-UTW-26 |
0.046 |
1.17 |
0.022 |
0.56 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-24 |
0.050 |
1.27 |
0.027 |
0.69 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-22 |
0.055 |
1.40 |
0.032 |
0.82 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-20 |
0.060 |
1.52 |
0.039 |
0.99 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-18 |
0.076 |
1.94 |
0.049 |
1.25 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-16 |
0.093 |
2.36 |
0.061 |
1.54 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-14 |
0.120 |
3.00 |
0.072 |
1.83 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-12 |
0.150 |
3.80 |
0.089 |
2.26 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-10 |
0.191 |
4.85 |
0.112 |
2.85 |
0.002 |
0.051 |
|
BH-MT-PTFE-1.7X-UTW-8 |
0.240 |
6.10 |
0.141 |
3.58 |
0.0025 |
0.064 |
|
Customized specifications are available on request. The tolerance of most specifications can be controlled within ± 0.025mm [0.001in] |
||||||
Custom specifications are available upon customer request. Tolerance for most sizes can be controlled within ±0.025 mm (0.001”)
Cross Reference:
ZEUS: Sub‑Lite‑Wall™ PTFE Heat Shrink Tubing
|
Property |
Specification Requirement |
Test Method |
Typical Value |
|
Tensile strength |
≥17.3MPa |
ASTM D2671 |
≥22MPa |
|
Elongation at break |
≥200% |
ASTM D2671 |
≥300% |
|
Heat shock |
No cracking |
ASTM D2671 |
No cracking |
|
Low temperature flexibility |
No cracking |
ASTM D2671 |
No cracking |
|
Volume resistivity |
≥1015Ω‧ cm |
ASTM D2671 |
≥1015Ω‧ cm |
|
Dielectric strength |
≥34kV/mm |
ASTM D2671 |
34 kV/mm |
|
Copper corrosion |
No corrosion |
ASTM D2671 |
No corrosion |
Written for microcatheter, guidewire and electrosurgical-device R&D and process engineers, OEM/ODM partners and sourcing teams. This FAQ focuses on selection, ultra-thin-wall processing practice, failure modes, sterilization, compliance boundaries and sourcing. All physical properties, dimensions, wall thicknesses and test values are published in the product datasheet and are intentionally not repeated here — refer to the BH-MT-PTFE-UTW product page for the full specification. Sub-Lite-Wall™ is a trademark of Zeus Industrial Products, Inc.; we are an independent manufacturer and are not affiliated with, or endorsed by, Zeus.
Q1. What should we verify before qualifying BH-MT-PTFE-UTW as a drop-in alternative for Sub-Lite-Wall™?
A1. Four checkpoints.
(1) Dimensional match at both ends of the shrink: the as-supplied ID must slide over your wire, mandrel or shaft with controlled clearance, and the fully recovered ID and recovered wall must land inside your design envelope — with ultra-thin-wall sleeves, wall-thickness tolerance directly consumes your profile budget, so cross-check our datasheet bands against your drawing rather than assuming identical tolerances.
(2) Confirm which version you need: a heat-recoverable version and a non-shrink version are both listed in the datasheet; they are not interchangeable in process terms.
(3) Processing prerequisites: PTFE recovery requires substantially higher temperatures than polyolefin or PVDF sleeves (see datasheet), so confirm your heating equipment and the temperature tolerance of everything under the sleeve.
(4) Run your own IQ/OQ/PQ before release; evaluation samples are available for exactly this qualification work. Trademark notice: Sub-Lite-Wall™ is a trademark of Zeus Industrial Products, Inc. We are an independent manufacturer and are not affiliated with, or endorsed by, Zeus; no Zeus endorsement applies to our products.
Q2. Which heating equipment suits ultra-thin-wall PTFE recovery, and what failure modes should we watch for?
A2. Use controlled, uniform heat: calibrated forced-air convection ovens, infrared tunnels or heated-mandrel stations with closed-loop control. Consumer heat guns or open flame create local hot spots that an ultra-thin wall cannot forgive. Failure modes frequently reported with UTW PTFE sleeves:
(1) pinholes — the critical defect class at this wall thickness, typically traced to local overheating, contaminant particles, or over-stretching during handling; pinholes show up later as dielectric breakdown or coating delamination, so add a pinhole/continuity inspection step;
(2) bubbles or blisters — PTFE is not hygroscopic, so bubbles usually come from air sealed in at the ends, substrate or mandrel outgassing, or too-rapid heating;
(3) whitening or chalky marks — stress whitening from kinking or tight bending, a serious warning sign on an ultra-thin wall rather than a cosmetic issue;
(4) crushing or imprinting of fragile micro-substrates — recovery force can deform fine wires and thin polymer tubes, so qualify on the real build;
(5) longitudinal shrink shift — heat symmetrically from the center outward and position the sleeve with allowance to avoid end exposure or splitting.
Q3. What should we know about contact with PEBAX, PFA, FEP, metals and medical adhesives?
A3. Temperature first: the recovery heat of PTFE is above the melt range of PEBAX, Nylon and PU, so do not recover the sleeve directly over these jackets unless the assembly is supported and the heat exposure is validated — for low-temperature jacket reflow, choose a lower-temperature process-aid sleeve from our range. Over metals — guidewire cores, hypotubes, ablation electrodes, endoscopic control wires — UTW PTFE is the classic fit, adding insulation and lubricity at minimal profile cost (see datasheet applications). PFA/FEP components tolerate elevated temperatures, but validate the exact stack because the recovery step reaches deep into their service range. On adhesion: PTFE is chemically inert and non-stick; adhesives, primers and outer-jacket materials will not bond to it without surface treatment such as sodium etching or plasma treatment. If your design requires bonding to or over the sleeve, plan that step explicitly or contact us to discuss options.
Q4. Any precautions for chemicals and disinfectants, and what material declarations are available?
A4. PTFE is among the most chemically resistant polymers in use, essentially unaffected by common hospital disinfectants, alcohols and most solvents, and resistant to corrosion by pharmaceutical solutions (see datasheet). If your device will see repeated exposure to a specific agent, share the chemistry and exposure cycle and we will support a compatibility assessment. On documentation: we support your material-declaration work with composition statements and ISO 10993 / USP Class VI material test reports. Note that fluoropolymers are receiving increased regulatory attention in some regions; if your market-access team needs substance-level declarations (for example for EU MDR 10.4 screening or PFAS-related customer questionnaires), raise this in the RFQ so the correct documentation is prepared from the start.
Q5. Which sterilization methods are supported, and what changes should we expect with repeated cycles?
A5. The datasheet states compatibility with high-pressure steam (autoclave), EtO, steam and dry heat sterilization — an important difference from standard-wall PTFE grades, where steam is not always a qualified method. Two practical notes.
(1) Gamma irradiation is not listed among the qualified methods for this grade; if your device is gamma-sterilized, treat it as a validation item and request samples for post-irradiation testing.
(2) Even with qualified methods, repeated cycles deserve verification on the recovered sleeve on your actual device: on ultra-thin walls, check dimensional stability, surface condition, and — where the sleeve serves as insulation — pinhole/dielectric integrity after the full intended number of cycles, because repeated thermal expansion against a metal substrate can drive end shrink-back and creep at bend points over time.
Q6. Where is ultra-thin-wall PTFE the right choice — and where is it NOT recommended?
A6. Well suited (see datasheet applications): coating, insulation and surface-smoothing of precision minimally invasive devices — microcatheters, balloon delivery systems, interventional guidewire sheaths, electrosurgical ablation electrodes and endoscopic control wires — wherever added profile must be near zero and low friction, corrosion resistance, high-temperature capability and electrical insulation matter. Use with caution or not recommended: joints under continuous dynamic flexing — PTFE is stiffer than FEP/PFA and an ultra-thin wall fatigues and stress-whitens sooner at tight repeated bend radii; high-abrasion sliding contact, where FEP or PFA sleeves generally wear better; any application expecting the sleeve to carry structural or tensile load — at this wall thickness it is a coating, not a structure; and recovery directly over low-melting thermoplastic jackets (see the compatibility question). If bending fatigue or abrasion dominates your design, tell us before design freeze and we will discuss alternatives openly.
Q7. Does ISO 10993 / USP Class VI compliance — or the published dielectric rating — mean our finished device is approved?
A7. No — and this distinction matters in audits. We supply component tubing only. Material-level compliance with ISO 10993 / USP Class VI supports, but does not replace or constitute, regulatory approval of your finished medical device: biological evaluation of the finished device (ISO 10993-1), sterilization validation, process validation (IQ/OQ/PQ) and risk analysis (ISO 14971) remain the device manufacturer’s responsibility. The same logic applies electrically: the dielectric properties in our datasheet are material-level test values, not an electrical safety certification of your instrument — on an ultra-thin wall this point is critical, because a single pinhole defeats the material rating. Dielectric withstand (hi-pot), leakage current, creepage and clearance verification on the finished device (for example under the IEC 60601 series where applicable) must be performed and documented by you on the final assembly, including after sterilization and aging. We do not claim performance beyond the published datasheet.
Q8. How should ultra-thin-wall tubing be stored, and does long-term storage change its properties?
A8. PTFE itself is exceptionally aging-resistant: no plasticizers to migrate, no moisture uptake, stable against UV and oxidation, and the datasheet assigns no fixed shelf life. For an ultra-thin wall, the real storage risks are mechanical, not chemical: keep spools in their packaging, clean, dry and away from heat sources; protect against crushing, kinking and sharp bending (deformation before recovery leaves whitening marks and causes uneven recovery or pinholes); minimize handling and airborne-dust exposure, since a contaminant particle embedded at this wall thickness can become a pinhole origin; apply first-in-first-out rotation. For lots stored long-term, run a quick recovery and visual check on a sample piece before releasing the lot to production, and include storage conditions in your incoming-inspection plan.
Q9. Do you support cutting, hole punching, custom dimensions or special tolerances?
A9. Cut-to-length supply is supported and is the most common secondary operation for this product. Customized specifications are available on request, and most sizes can be held to tight dimensional tolerances (see datasheet) — tell us which tolerance actually matters functionally (recovered ID, recovered wall, or length) so capability is confirmed against the right dimension. Hole punching or similar features: PTFE can be machined, but any feature cut into an ultra-thin wall changes local recovery behavior and creates split-initiation points, so we evaluate such requests together with your process team before committing. Describe the requirement in your RFQ and we will confirm feasibility.
Q10. How do samples and the ramp from trials to mass production work?
A10. Evaluation samples of standard sizes are available for recovery-window qualification on your real equipment and substrate — with UTW PTFE this step is essential, because the wall forgives nothing and your heating recipe should be finalized with sample material before design freeze. We then support pilot batches through to mass production, with lead times confirmed at quotation. Many customers approach us while dual-sourcing against an incumbent fluoropolymer supplier after experiencing long lead times or allocation risk on branded ultra-thin-wall PTFE; if that is your situation, share the reference specification and we will map the closest equivalent for side-by-side trials.
Q11. What engineering information should an RFQ include?
A11. For a fast and accurate quotation, please provide: required size (as-supplied ID and/or fully recovered ID) and the recovered wall-thickness requirement, including which tolerance is functionally critical; whether you need the heat-recoverable or the non-shrink version; quantity and estimated annual volume; supply form (spool or cut length, with tolerance and edge-quality requirement); the application and what sits under the sleeve (wire/hypotube/electrode material and OD, or polymer substrate); the profile budget the recovered sleeve may add; your heating equipment type and available process temperature; whether the sleeve must be bonded to or overmolded (i.e., whether surface treatment is planned); sterilization method and number of cycles the device must survive; electrical requirements if used as insulation (operating voltage, hi-pot level of the finished device, and whether pinhole inspection is required); secondary operations (cutting, holes); compliance documentation required (ISO 10993 / USP Class VI material reports, composition declarations); and target price, delivery terms and destination.
Q12. What should we know about material declarations, MDM documentation and FDA master files?
A12. Practical points.
(1) We provide material-level documentation — composition statements and ISO 10993 / USP Class VI material test reports — for your technical file, EU MDR documentation or supplier-qualification records.
(2) Where a device master file (MAF) reference is the right mechanism, we can discuss authorization letters so your regulatory team can reference our material data in your submission; scope is agreed case by case.
(3) What we do not do: we make no claim or commitment on behalf of your finished device — our material documents imply no device-level FDA clearance, no CE conformity, and no device-level biological or electrical safety approval.
(4) Change control: if your regulatory filing requires notification agreements for material or process changes, raise this before design freeze so it is covered in the supply agreement.
(5) Trademark note for your documentation: Sub-Lite-Wall™ is a trademark of Zeus Industrial Products, Inc.; referencing a third-party trademark in your internal equivalence matrix is normal engineering practice, but our products are independently manufactured and carry no Zeus affiliation or endorsement.