|
ITEM
|
INCH
|
MM
|
|
INSIDE DIAMETER (ID )
|
0.01 -0.40
|
0.30 – 10.0
|
|
ID TOLERANCE
|
± 0.001 – 0.003
|
± 0.025 – 0.076
|
|
NOMINAL WALL THICKNESS
|
0.001 – 0.003
|
0.025 – 0.076
|
|
WALL TOLERANCE
|
± 0.0005
|
± 0.0127
|
|
CUT LENGTH
|
39-78
|
1,000-2,000
|
|
Property
|
Specification Requirement
|
Test Method
|
Typical Value
|
|
Etching Angle
|
<70°
|
–
|
60°
|
|
Flammability
|
V0
|
UL94
|
V0
|
|
Chemical Resistance
|
excellent
|
–
|
excellent
|
|
Heat shock
|
No cracking
|
ASTM D2671
(400˚C/4 hrs)
|
No cracking
|
|
Low temperature flexibility
|
No cracking
|
ASTM D2671
(-65˚C/4 hrs)
|
No cracking
|
|
No heavy metals contained
|
Q1. What is a medical grade free extruded etched PTFE liner?
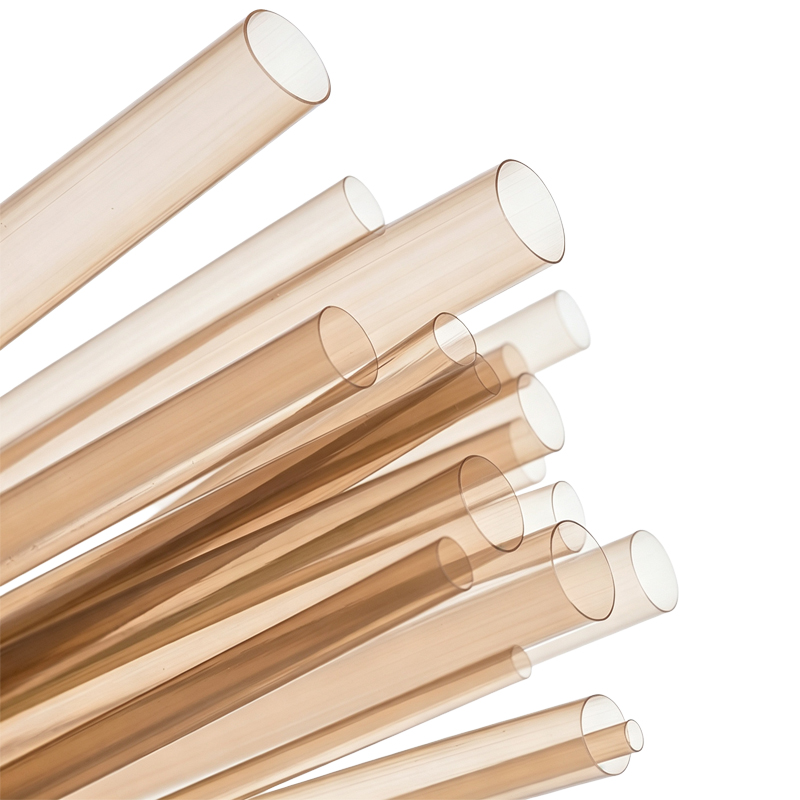
A1. A free extruded PTFE liner is a thin-walled polytetrafluoroethylene tube produced by paste extrusion without a supporting mandrel-forming step in the final sizing, giving a uniform, concentric wall. “Etched” means the outer surface has been chemically treated (typically with a sodium naphthalenide solution) to raise surface energy from 18 dynes/cm to >50 dynes/cm, enabling adhesive or thermal bonding to the catheter jacket. The inner (blood/device-contacting) surface retains PTFE’s native ultra-low coefficient of friction (0.04–0.10), while the outer surface becomes bondable. In catheter construction it serves as the innermost layer of a multilayer shaft — a construction catheter R&D engineers describe as an outer Pebax jacket encapsulated over a surface-etched PTFE liner to get low friction on the inside.
Q2. What is the difference between free extruded and mandrel (paste) extruded PTFE liners?
A2. Both are paste-extrusion routes — PTFE cannot be melt-extruded like Pebax, nylon, or FEP because its melt viscosity is too high; it requires paste extrusion followed by high-temperature sintering. In mandrel-based extrusion the tube is formed and sintered on a precision mandrel, which gives excellent ID control but limits length and adds mandrel insertion/removal steps. Free extrusion produces the tube unsupported, which suits continuous, high-volume production of long lengths and, per industry literature, can enhance yield strength and axial strength through controlled fibril orientation. Free extruded liners are well suited to applications where the liner will be laminated/bonded into a braided or jacketed shaft and the final ID is governed by the assembled construction rather than the liner alone.
Q3. How does PTFE etching work, and why is it necessary?
A3. PTFE’s extremely low surface energy (18 dynes/cm) — the same property that gives it lubricivity — makes it essentially non-stick, so adhesives and molten jacket polymers (Pebax, nylon, TPU) will not wet or bond to it. Chemical etching with a sodium-based solution (commonly sodium naphthalenide) removes fluorine atoms from the surface and introduces oxygen-containing functional groups, raising surface energy above 50 dynes/cm and creating a microscopically rough surface for mechanical interlock. This is the standard pretreatment before jacketing; engineers on Reddit consistently flag PTFE bonding as the #1 processing challenge with the material.
Q4. How do I bond an etched PTFE liner to Pebax, nylon, or TPU jacket materials?
A4. Two mainstream approaches are used, and both are discussed extensively by engineers: (1) Chemical etching of the liner outer surface followed by adhesive lamination or reflow — the etched surface accepts adhesives and also improves mechanical interlock with the jacket during thermal reflow. (2) Tie-layer technology — a thin thermoplastic elastomer layer (e.g., modified Pebax or polyurethane) is applied to the PTFE outer surface; the tie layer fusion-bonds to PTFE under heat and pressure and its outer surface bonds readily to the jacket. Tie layers are particularly valuable for ultra-thin-wall constructions where the etched surface alone may not provide sufficient bonding area. Choice depends on your jacket material, reflow process, and whether the device will see flex fatigue.
Q5. What bonding performance should I expect, and how is it verified?
A5. Bond strength is typically verified by peel or pull testing of the liner–jacket interface after reflow/lamination, plus contact-angle measurement on the etched surface to confirm surface energy (>50 dynes/cm or equivalent wetting). Suppliers of etched liners commonly certify etch quality via contact angle and peel-strength testing per lot. Device-level validation should include simulated-use flex fatigue and burst/kink testing of the full multilayer construction, because delamination risk escalates with each added layer in a 4–6 layer catheter shaft.
Q6. Is etched PTFE biocompatible for blood-contacting applications?
A6. Yes. Medical-grade PTFE is a well-established blood-contacting material with a clinical history dating to the 1950s; it is non-thrombogenic relative to most polymers, chemically inert, and dimensionally stable (moisture absorption <0.01%). Device-level biocompatibility evaluation per ISO 10993-1 (cytotoxicity, sensitization, irritation, hemocompatibility as applicable) is still required for the finished device — material-level compliance (e.g., USP Class VI resin) does not substitute for device-level testing. Note that etching is applied to the outer surface only; the inner luminal surface remains virgin PTFE.
Q7. What dimensional tolerances can be held on free extruded etched PTFE liners?
A7. Free extrusion of PTFE can achieve very thin walls — industry literature reports walls down to roughly 0.0005″ (12.7 µm) for paste-extruded PTFE liners with tolerances on the order of ±0.0003″, and thinner (down to 0.0003″ / 7.6 µm) with specialized processes. Typical catheter-shaft lumen tolerance in finished multilayer constructions is around ±0.001″, and OD tolerance around ±0.002″–±0.003″ depending on jacket and braid configuration. Because PTFE absorbs essentially no moisture, etched liners are dimensionally stable through manufacturing, storage, and use — unlike nylon, which absorbs 0.6–1.0% moisture and can drift in humid environments.
Q8. Which catheter applications are etched PTFE liners best suited for?
A8. PTFE liners are the default choice where lubricity is critical: guide catheters, diagnostic angiographic catheters, neurovascular microcatheters, steerable/deflectable catheters, introducer sheaths, and stent/balloon delivery systems — essentially any device where guidewires or implants must pass through the working channel with minimal force. Engineers note that PTFE “earned its place as a gold standard” for tortuous-path, demanding catheter applications. For larger-diameter peripheral and urological devices where extreme miniaturization matters less, Pebax, nylon, or FEP may be more cost-effective; PTFE is sometimes reserved for distal tip segments in those cases.
Q9. How is etch quality and liner quality inspected incoming and in-process?
A9. Standard incoming and in-process checks include: (1) contact-angle / surface-energy measurement on the etched outer surface (dyne level or water contact angle) to verify etch activation; (2) visual inspection under magnification for etch uniformity, discoloration (over-etching shows as a brownish tint, which is normal for sodium-etched PTFE), scratches, and pinholes; (3) dimensional verification — ID, OD, wall thickness, and concentricity by laser micrometer or vision system; (4) peel-strength testing of bonded samples per lot; (5) for the finished device, burst pressure, leak testing, and simulated-use flex fatigue to catch incipient delamination. Etch consistency between batches is a common supplier-quality discussion point among engineers.
Q10. What are the most common failure modes, and how are they prevented?
A10. The failure modes engineers discuss most: (1) Delamination of the liner from the jacket or braid — mitigated by verified etch quality, tie layers for ultra-thin walls, and validated reflow parameters; (2) Kinking or lumen collapse at tight bend radii — managed by wall thickness selection, braid/coil reinforcement, and anisotropic vs. isotropic liner choice; (3) Scratching or abrasion of the liner during guidewire passage — PTFE is relatively soft and susceptible to creep/cold flow, so support from the outer shaft is essential; (4) Bond-line failure after sterilization or flex fatigue — screened by device-level simulated-use testing; (5) Processing hazards — PTFE fumes during overheating are toxic, and sodium-etch chemistry requires strict handling controls. A recurring theme in engineering forums: PTFE’s low-friction advantage and its bonding difficulty are the same property — process control around the etched surface is the critical control point.
Q11. How does sterilization affect etched PTFE liners?
A11. PTFE is among the most sterilization-compatible catheter polymers: it tolerates EtO, steam autoclave (121–134°C), gamma, e-beam, and vaporized hydrogen peroxide without significant degradation — a key advantage over nylon and Pebax, which degrade under gamma/e-beam and absorb moisture during autoclaving. This makes PTFE-lined catheters suitable for reusable devices requiring repeated autoclave cycles. Always verify the full assembled device (liner + jacket + adhesive) through the chosen sterilization cycle, since the jacket or bond line is usually the limiting factor, not the PTFE.
Q12. What about PFAS regulatory pressure — should I be planning a post-PTFE strategy?
A12. This is an increasingly frequent question in engineering discussions. Medical-grade PTFE remains considered safe and essential by FDA, but as a fluoropolymer it falls under the broader PFAS scrutiny (ECHA restrictions, EPA/MDR attention), and supply chains are beginning to shift. Alternatives being evaluated include UHMWPE liners (low friction, ISO 10993-proven, but lower reflow temperature 130–150°C can cause lumen collapse during Pebax jacket reflow, and it softens/flows during processing unlike PTFE), PFAS-free lubricious additives for jackets, and hybrid PI/PTFE composites. The consensus in engineering forums is not to replace PTFE immediately, but to evaluate alternatives early in development so material decisions are not forced later. For new designs with 5–10 year lifecycles, dual-track material qualification is prudent.