Founded in 2010, FLYPOWER is a high-tech enterprise specializing in the research, development, production, and sales of polymer materials. Leveraging its core technological strengths and starting with heat-shrink materials, the company established its Medical Division in 2018, expanding its business and product portfolio into the fields of medical devices and catheters, with the mission of becoming a globally leading supplier of materials for interventional medical devices.
联系我们 No. 77, Bao Nan Road,Nan Lian Community,Long Gang Street,Long Gang District, Shenzhen, Guangdong,518116,China (+86)755 2917 9250 [email protected]
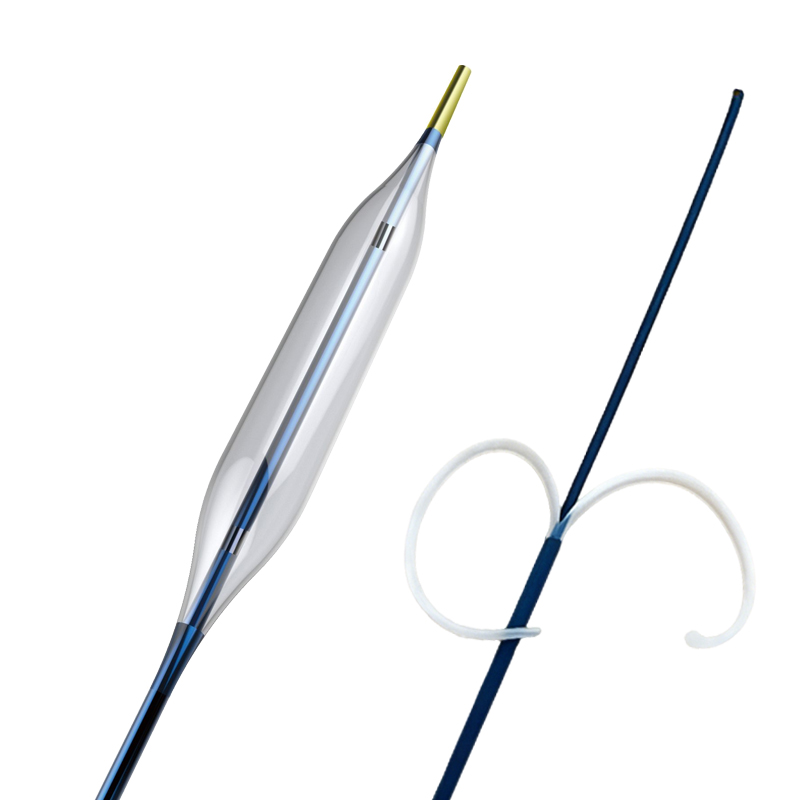
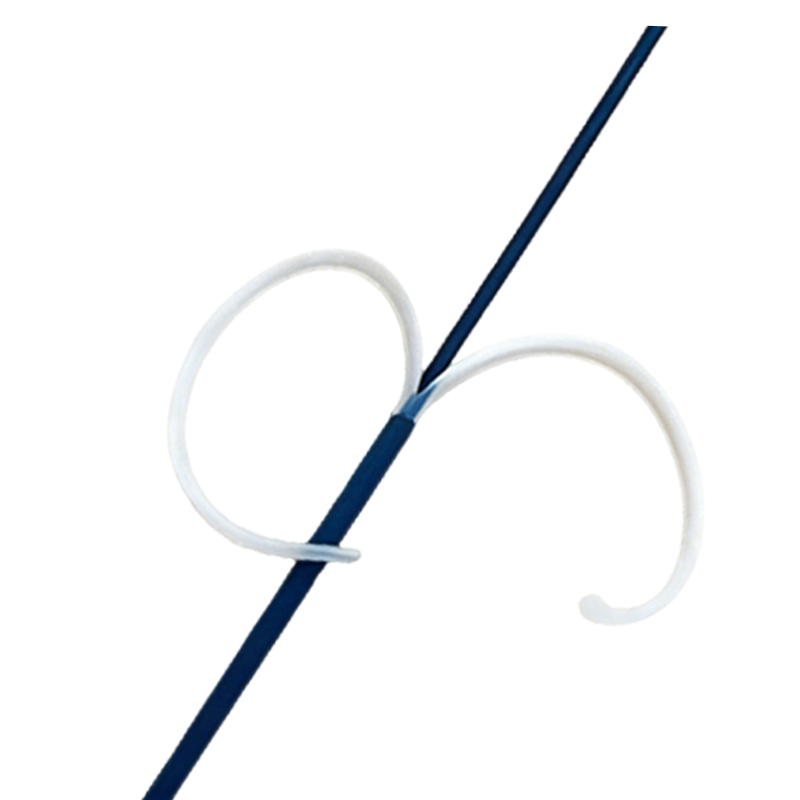
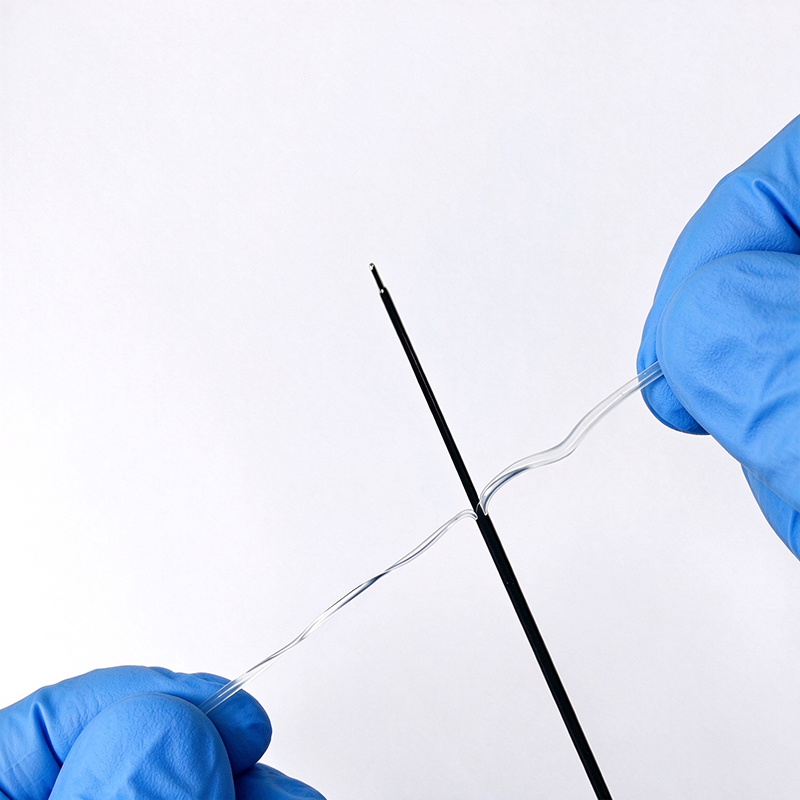
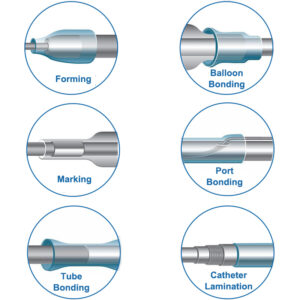
BH-2(PMT) is made by medical grade modified polyolefin, it can be quickly and easily peeled the heat shrink tube away from the recovered shaft while it is softening by heat. Well-suited for laser-welding operations of stents and balloons, hot jaw bonding. Widely using for the process of aid production of catheter lamination, balloon tacking, tube bonding and tube forming.
Shrink Ratio: 2:1
Removes easily after application, good axial tear propagation
Compatibility with gamma rays and ETO sterilization
Packing by plastic spools double bag packaging
Work temperature:-45°C ~ +105°C
Minimum shrink temperature: 70℃
Fully recovery temperature: +130℃~ +260℃
Special design it could withstand Max. 260℃ in the recovery process
Compliant with ISO 10993 and USP Class VI, no heavy metals
|
Model |
Size |
As Supplied ID |
Recovered ID (Max) |
Recovered WT |
Package (M/Spool) |
|||
|
Inch |
mm |
Inch |
mm |
Inch |
mm |
|||
|
BH-2(PMT)-0.6 |
1/42 |
0.028 ± 0.005 |
0.71±0.10 |
0.011 |
0.28 |
0.010 ± 0.002 |
0.25±0.05 |
200 |
|
BH-2(PMT)-0.8 |
1/32 |
0.040 ± 0.005 |
1.02±0.13 |
0.014 |
0.36 |
0.011 ± 0.002 |
0.28±0.05 |
200 |
|
BH-2(PMT)-1.2 |
3/64 |
0.055 ± 0.005 |
1.40±0.13 |
0.020 |
0.51 |
0.016 ± 0.003 |
0.41±0.08 |
200 |
|
BH-2(PMT)-1.6 |
1/16 |
0.072 ± 0.005 |
1.83±0.13 |
0.028 |
0.71 |
0.020 ± 0.003 |
0.51±0.08 |
200 |
|
BH-2(PMT) -2.0 |
5/64 |
0.078 ± 0.005 |
2.21±0.13 |
0.033 |
0.85 |
0.020 ± 0.003 |
0.51±0.08 |
100 |
|
BH-2(PMT)-2.4 |
3/32 |
0.107 ± 0.008 |
2.72±0.20 |
0.041 |
1.04 |
0.020 ± 0.003 |
0.51±0.08 |
100 |
|
BH-2(PMT)-3.2 |
1/8 |
0.140 ± 0.010 |
3.56±0.25 |
0.057 |
1.45 |
0.020 ± 0.003 |
0.51±0.08 |
100 |
|
BH-2(PMT)-4.8 |
3/16 |
0.205 ± 0.010 |
5.21±0.25 |
0.087 |
2.21 |
0.020 ± 0.003 |
0.51±0.08 |
50 |
|
BH-2(PMT)-6.4 |
1/4 |
0.275 ± 0.015 |
6.99±0.38 |
0.118 |
3.00 |
0.025 ± 0.003 |
0.64±0.08 |
25 |
|
BH-2(PMT)-9.5 |
3/8 |
0.415 ± 0.020 |
10.54±0.51 |
0.170 |
4.30 |
0.025 ± 0.003 |
0.64±0.08 |
Cut in length |
Customized dimensions and heat shrink ratio for your special applications on request.
Cross Reference :
Tyco Connectivity / Raychem MT-LWA
Applications:
|
Property |
Test Method |
Typical Data |
|
Longitudinal change |
ASTM D 2671 |
-10%~10% |
|
Concentricity as supplied |
ASTM D 2671 |
≥ 70% |
|
Tensile strength |
ASTM D 2671 |
≥ 10.3 Mpa |
|
Elongation at break |
ASTM D 2671,20″/minute |
≥ 200% |
|
Secant modulus (expanded) |
ASTM D 2671 |
≤ 2.5 x10⁴ Mpa |
|
Elongation at break after aging |
ASTM D 2671(175˚C/168 hrs) |
≥ 100% |
|
Electrical dielectric strength |
ASTM D 2671 |
≥19.7kV/mm |
|
Dielectric withstand |
ASTM D 2671(AC3000V/60Hz) |
60 Seconds no breakdown |
|
Heavy metals analysis |
USP XXII Physiochemical tests-plastic |
≤ 1 ppm(total of all metals) |
Written for catheter R&D and process engineers, OEM/ODM partners and sourcing teams. This FAQ focuses on replacement, hot peeling, thermal processing and compliance practice. All physical properties, dimensions and test values are published in the product datasheet and are intentionally not repeated here — refer to the BH-2(PMT) product page for the full specification.
Q1. What should we verify before qualifying BH-2(PMT) as a drop-in alternative for MT-LWA?
A1. Four checkpoints.
(1) Dimensional match: the as-supplied ID must slide over your catheter build, and the recovered ID and recovered wall must deliver the radial compression your process needs — cross-check against our datasheet rather than assuming identical tolerance bands.
(2) Thermal window match: confirm that the recovery temperature window of the sleeve (see datasheet) matches the melt and reflow requirements of your substrate stack; this grade is designed to withstand the upper end of its recovery window, which is useful for higher-melting substrates and laser or hot-jaw processes.
(3) Hot-peel validation on your real build: run trial cycles on actual shafts and verify clean, one-piece removal at your real process timing.
(4) Complete your own process validation (IQ/OQ/PQ) before production release. Evaluation samples are available for exactly this purpose.
Q2. What practical differences should we expect versus MT-LWA?
A2. BH-2(PMT) serves the same function class: a peelable, medical grade modified-polyolefin process-aid sleeve that is removed after reflow, welding or bonding. Differences to plan for: dimensional tolerance bands follow our own datasheet; the standard color is clear; the tubing is supplied on plastic spools in double-bag packaging; and customized dimensions and shrink ratios are available on request. Qualifying this second source typically addresses the long distribution lead times, high small-quantity pricing and single-source risk frequently reported for branded peelable sleeves. Trademark notice: MT-LWA is a trademark of TE Connectivity. We are an independent manufacturer and are not affiliated with, or endorsed by, TE Connectivity; no TE endorsement applies to our products.
Q3. How does the hot-peel process work, and what failure modes should we watch for?
A3. This grade is designed to be peeled while it is still hot and softened by the process heat: in this state the material modulus is low and interfacial adhesion has not fully set, so the sleeve tears open axially with low peel force. Hot removal also avoids a known risk of cold removal — cutting off a cooled, tight sleeve with blades can scratch delicate compliant balloons and thin catheter jackets. Standardize the peel step in your work instruction: a defined start point (cut or nick), an axial pull direction, and a defined timing after the heat step. Common failure modes reported with peelable sleeves in catheter manufacturing: (
1) fragment residue on the shaft, usually linked to over-processing or a poor peel start;
(2) mid-peel tearing, often when the sleeve has been overheated and its tear propagation degraded;
(3) sleeve sticking to the jacket and picking up substrate material when peeled, caused by excessive temperature or dwell. Prevention: qualify the minimum heat and dwell that still achieve full reflow, peel at the qualified timing, and add a post-peel visual inspection step.
Q4. How do we suppress bubbles during reflow with this sleeve?
A4. Bubbles in catheter reflow usually come from four sources: moisture in hygroscopic substrates, air entrapment during shrinking, polymer degradation from excessive heat, and outgassing from the mandrel. Practical countermeasures: dry PEBAX, Nylon and PU components thoroughly before processing; manage the shrink direction and speed so air can escape instead of being sealed in at the ends; use the lowest temperature and dwell that achieve full reflow; and keep mandrels clean and free of drawing oil or solvent residue. The sleeve is specially designed to withstand the upper end of its recovery window (see datasheet), giving you headroom when processing higher-melting substrates — but always qualify the window on your real stack rather than running hotter than necessary.
Q5. Is the sleeve compatible with reflow and welding of PEBAX, Nylon and PU substrates?
A5. These are the most common catheter jacket materials, and the sleeve is intended for exactly this type of reflow, fusion-welding and bonding work — it is well suited for laser-welding operations of stents and balloons and for hot jaw bonding. Because substrate melt ranges vary widely with polymer family and durometer, match the process window to your actual stack: confirm that full sleeve recovery is achieved at a temperature your substrates tolerate, and validate on the exact resin grade and hardness you run in production. Trial spools for window development are available on request.
Q6. Any precautions regarding contact with catheter substrates, cleaning agents or process aids?
A6. Keep contact surfaces clean: mandrel drawing oils, isopropyl alcohol that has not flashed off, and lubricant or adhesive residues on the build can all interfere with reflow quality and hot peeling. If your process uses cleaning agents, release aids or primers in contact with the sleeve, share the chemistry with us and we will run a compatibility assessment before your design freeze. The material contains no heavy metals (see datasheet), which simplifies your material declaration work.
Q7. Do gamma or EtO sterilization affect peel performance?
A7. The datasheet states compatibility with gamma irradiation and EtO sterilization. As a process aid, the sleeve is normally removed before the finished device is sterilized; if your workflow sterilizes components or subassemblies while the sleeve is still in place, validate peel behavior after sterilization on a lot basis, since radiation and EtO exposure can shift polymer properties. Repeated sterilization of the sleeve itself is not a standard use case — if you require it, treat it as a validation item and contact us for supporting samples.
Q8. Which process-aid applications is this sleeve suited for — and where is it NOT recommended?
A8. Suited: laser-welding operations of stents and balloons, hot jaw bonding, catheter lamination, balloon tacking, tube bonding and tube forming. NOT recommended: as a permanent on-device component (insulation, strain relief or an implantable sleeve that stays on the device — choose a permanent medical grade tubing from our range instead); as a substitute for adhesive-lined sealing; or where the process temperature exceeds the window published in the datasheet. Note also that this grade is designed for hot peel — if your workflow requires peeling after cooling without additional heat, ask us about our BH-2(PMT)-LS variant.
Q9. Does ISO 10993 / USP Class VI material compliance mean our finished device is approved?
A9. No. We supply component tubing only. Material-level compliance with ISO 10993 / USP Class VI supports — but does not replace or constitute — regulatory approval or clearance of the finished medical device. Biological evaluation of the finished device (ISO 10993-1), sterilization validation, process validation and risk analysis (ISO 14971) are the responsibility of the device manufacturer. As a process aid the sleeve is normally removed before the finished device is completed, but any residual-contact evaluation remains part of your device-level assessment. We do not claim performance beyond the published datasheet.
Q10. How should the tubing be stored, and can storage affect peel performance?
A10. Keep the spools in their double-bag packaging, stored cool, dry and away from direct sunlight, UV and heat sources; use first-in-first-out rotation. The datasheet does not assign a fixed shelf life. Because peel performance is the critical functional property of a process-aid sleeve, we recommend a quick hot-peel behavior check on lots that have been stored for an extended period before releasing them to production, and including storage conditions in your incoming-inspection plan.
Q11. Do you support secondary processing such as cutting, and how do samples and the ramp to production work?
A11. Yes — cut-to-length supply is available, and customized dimensions and heat shrink ratios can be developed for special applications (see datasheet). Other secondary operations such as marking can be evaluated on request; tell us your requirement in the RFQ. Evaluation samples of standard sizes are available for process-window development and hot-peel validation; we then support pilot batches through to mass production, with lead times confirmed at quotation.
Q12. What engineering information should an RFQ include?
A12. To receive a fast and accurate quotation, please provide: required size (as-supplied ID and/or recovered ID, plus any wall-thickness requirement); quantity and estimated annual volume; supply form (spool or cut length with tolerance); the process step the sleeve supports (e.g., laser welding of stents or balloons, hot jaw bonding, catheter lamination, balloon tacking, tube bonding or forming) and the substrate materials involved (e.g., PEBAX, Nylon, PU, with durometer if available); your process temperature range and equipment type; whether components will be sterilized with the sleeve in place, and by which method; any customization needs (special dimensions, shrink ratio, cut lengths, marking); compliance documentation required (e.g., ISO 10993 / USP Class VI material test reports); and target price, delivery terms and destination.